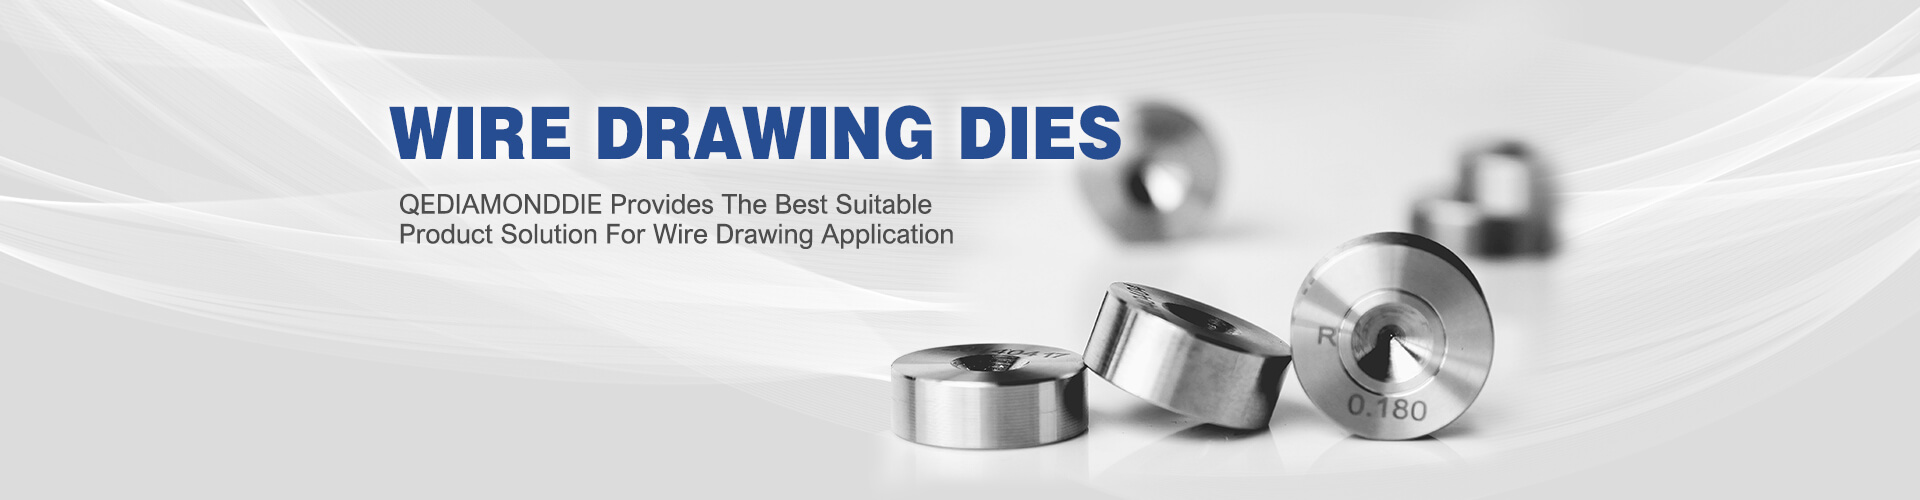
1: The cable drawn by the wire drawing die is broken
| Reason | Solution |
| The joint is not strong | Adjust the current, energization time, and pressure of the butt welding machine to improve the welding quality |
| There are impurities in the wire | strengthen the acceptance of raw materials |
| Unreasonable mold matching | Solution: adjust the wire drawing die to eliminate the phenomenon of large and small deformation process |
| The shape of the drawing die hole is incorrect or not smooth | Repair the mold strictly according to the standard, the sizing area should not be too long, and ensure the smoothness of the mold hole |
| The back pull force is too large | adjust the number of coils on the drum |
| Pressure line on the drum | Adjust the number of coils on the drum to correct the worn drum |
| Poor lubrication | check the lubrication system, determine the composition and temperature of the lubricant |
2: The size and shape of the drawing die are wrong
| Reason | Solution |
| Die hole wear | measure the wire diameter frequently, and replace the mold when it is found to be out of tolerance |
| The wire is thin | Adjust the matching mold to improve the lubrication effect |
| Using the wrong mold | Measure the wire diameter after threading |
| The wire is scratched | Check the quality and lubrication of the die hole |
| The mold is skewed | Pay attention to straightening the upper mold, and overhaul the mold base |
3: Wire drawing die scratches, bruises, scratches
| Reason | Solution |
| There is a jumper phenomenon on the tapered drum | smooth the surface of the drum wheel and check the correct angle |
| There are grooves on the drum | Remove the drum and repair the polishing |
| There is a damaged line on the device | The interface of the drum wheel is uneven, and the rotation of the guide wheel is not flexible |
| The coils collide with each other | The reels should be placed in the word "T", and they should be separated from each other during transportation. |
| The ground is uneven | Renovate the ground and lay steel plates |
| The take-up line is too full | stick to the post, concentrate on, and order according to the regulations. |
4: Continuous scratches on the mold
| Reason | Solution |
| The wire is scratched | Check the parts that are in contact with the wire, such as guide wheels and wire bars |
| The die hole is not smooth and has defects | Strengthen the repair and management of molds, and unqualified molds will not be put on the machine |
| The temperature of the lubricating fluid is too high | Strengthen cooling, and use forced cooling if necessary |
| The lubricating area of the die hole is blocked | Filter the lubricating fluid to eliminate metal shavings and various impurities in the lubricating fluid. |
| The lubricant has high alkali content and is not clean | regular testing, maintain the composition of the lubricant, and ensure its cleanliness |
5: Wire drawing die oxidation, water stains, oil stains
| Reason | Solution |
| Insufficient lubrication, high temperature of lubricating fluid | Ensure sufficient supply of lubricating fluid and strengthen cooling of lubricating fluid |
| Splash of lubricating fluid | block the splashing part, use felt to wipe the line at the exit of the finished line |
| The storage site is not clean, and the oily gloves dirty the wire | Adhere to 5S management to ensure the cleanliness of the workplace |